Line Boring & Bore Welding
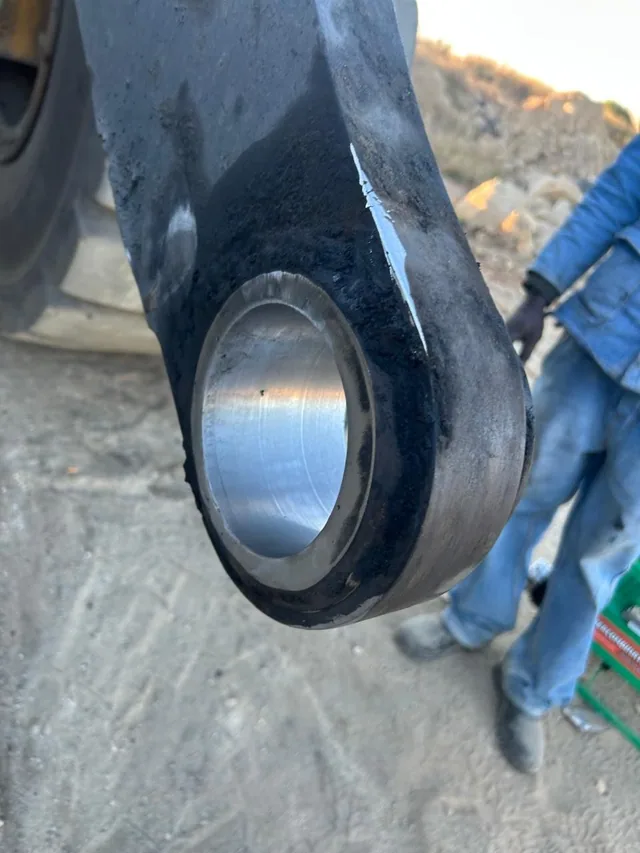
Worn pin bores welded up and machined back to size in place, on the boom, the chassis or the bucket.
What the work involves
Every pin joint on an excavator, loader or dozer wears. The bore goes oval, the pin knocks, the bush spins, and the slop works its way through the whole linkage until the machine loses accuracy and the parent casting starts to crack.
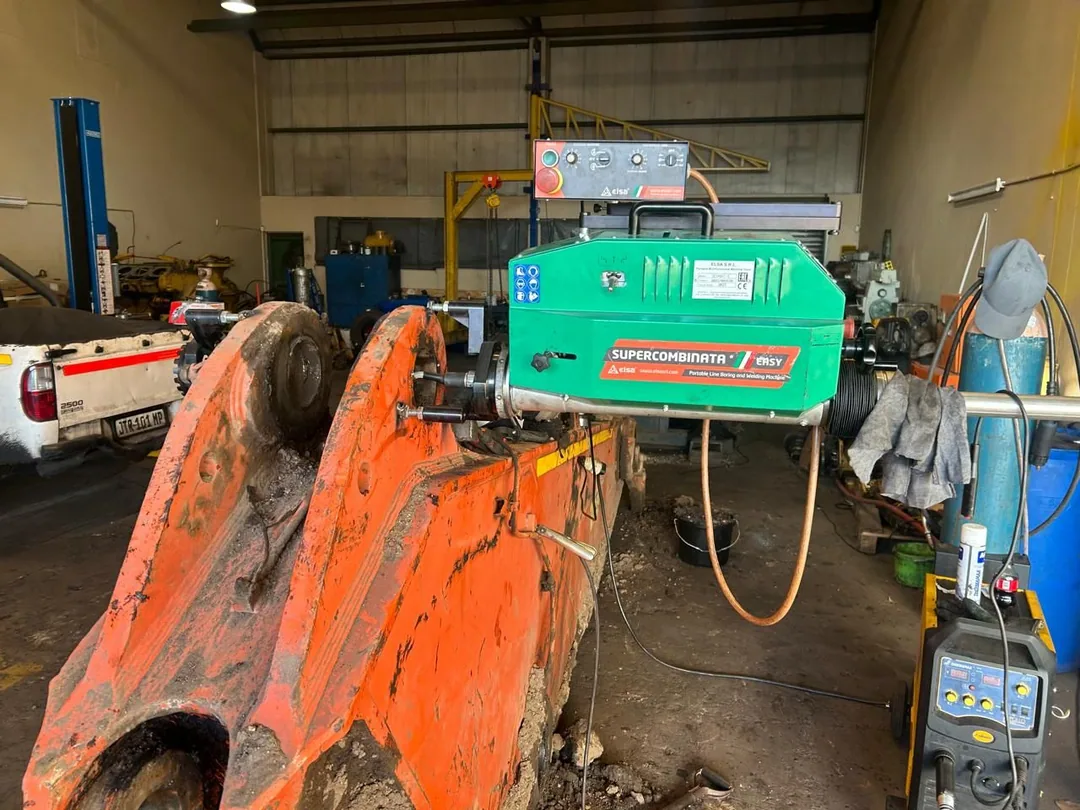
The repair is to put the metal back and cut it true. The bore is welded up to restore material, then a portable boring bar is clamped to the structure itself, aligned to the original centre line and used to machine the bore back to the drawing size. Because the equipment travels to the machine, the boom or chassis does not have to be cut out and freighted to a machine shop.
Work is carried out in our workshop where the component can come in, and on site where it cannot. Paired lugs are bored on one setup so the two bores stay concentric, and new bushes are pressed and measured before the joint is pinned back up.
- Division
- Heavy Mechanical
- Availability
- Workshop and on site
- Method steps
- 5
- Sectors served
- 3
- Base
- Middelburg
What this actually changes for your operation
The machine does not leave site
The boring equipment is portable and clamps to the structure being repaired, so a worn boom is fixed where it stands instead of being cut out and carted to a machine shop.
Metal replaced, not packed out
The bore is welded back up and cut to size. Oversize bushes and weld-and-hope shims move the problem along a few hundred hours; restoring the bore ends it.
Paired lugs bored on one setup
Both sides of a joint are machined from the same alignment, which is what keeps the bores concentric and stops the new pin binding.
Cracking headed off
Slop in a pin joint loads the parent casting in a way it was never designed for. Catching the bore early is cheaper than a structural repair later.
How the work runs, step by step
- 01
Measure and assess
Same dayPin and bore measured, wear pattern recorded and the joint checked for cracking before anything is committed to.
- 02
Strip and prepare
Per scopePin and bush removed, the bore cleaned back to sound metal and the structure supported so nothing moves during the repair.
- 03
Bore welding
Per scopeMaterial deposited back into the bore under a controlled pass sequence, building the wall up past finished size.
- 04
Line boring
Per scopeBoring bar clamped and aligned to the original centre line, then the bore machined back to the drawing dimension and finish.
- 05
Bush, pin and hand back
Same dayNew bush pressed, bore and pin measured against specification, joint reassembled and the recorded sizes handed over.
The repair, as it happens
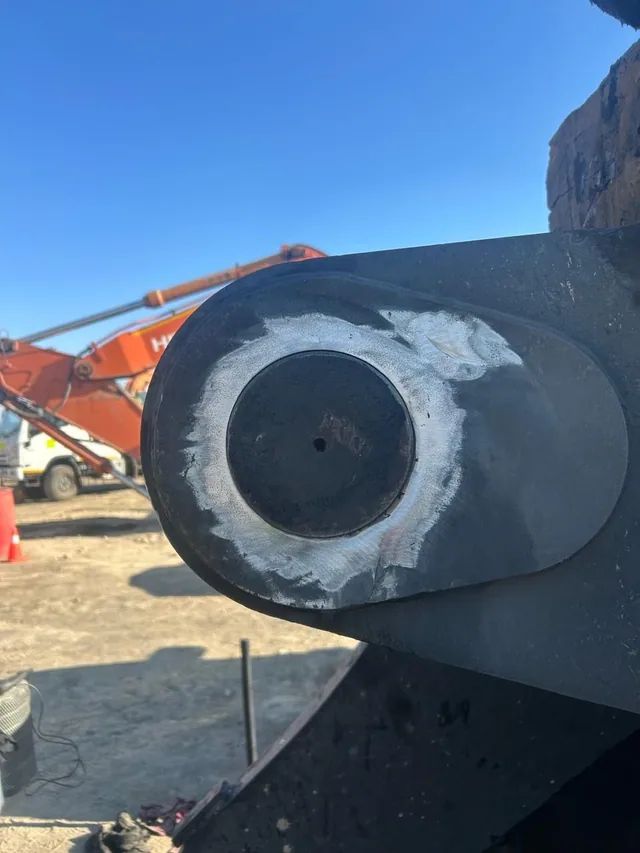
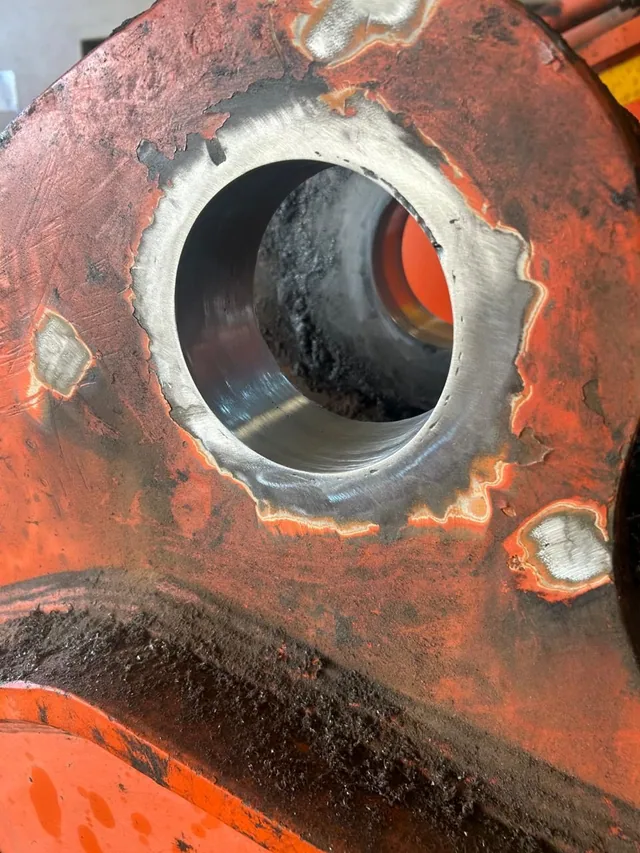
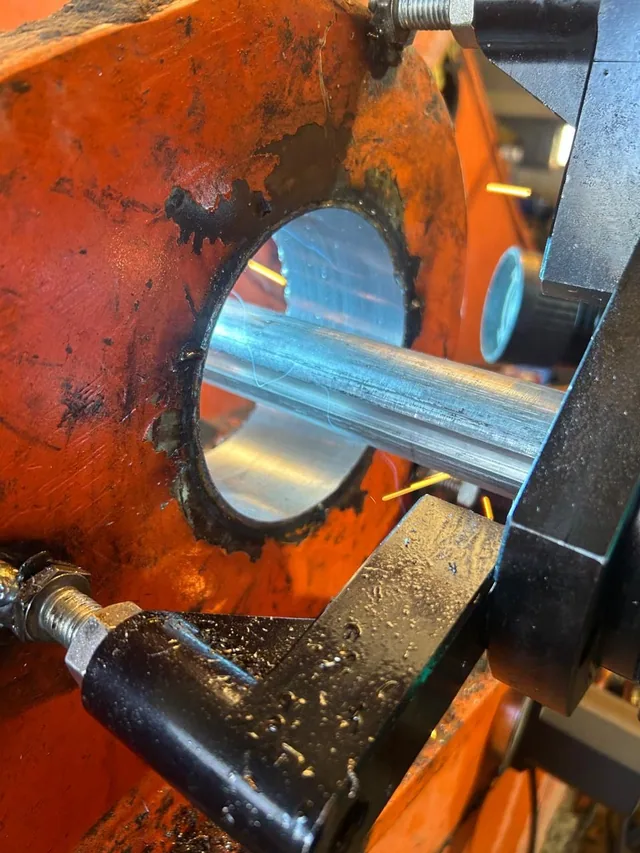
The rig, set up and runningThe boring unit clamped to the boom, aligned and cutting. Nothing was removed from the machine to get here. Bore welding, first passesWeld metal laid into the worn bore under a controlled pass sequence, building the wall back past finished size. Looking down the boreThe same weld seen from the open end, running an even bead around the full circumference. Welding head on the boomThe welding head driven by the same unit that will later carry the cutting tool, so the two share one alignment. Boring bar set to the centre lineThe bar mounted through the joint and trued to the original bore centre before a cut is taken. Taking the cutSwarf coming off a continuous cut. A clean, unbroken chip is what a correctly fed bore looks like. Machining back to sizeThe head working through the joint, with the cuttings collecting below the repair.
What we bring to it
Portable line boring unit
Clamps to the structure, aligned to the original bore centre line
Bore welding head
Rotating deposit of weld metal to rebuild a worn bore
Mobile power and welding plant
Carried to site so the repair runs where the machine stands
Measuring equipment
Bore gauges and micrometers, with sizes recorded before and after
Press and bush tooling
Fitting bushes without distorting the restored bore
What is in place before work starts
Structures supported and cribbed before any pin is driven out
Hot work permits, gas testing and fire watch before welding on site
Machine isolated and locked out, with hydraulics depressurised
Fume extraction in the workshop and respiratory protection in the field
Where this service is used
Usually bought alongside
Need line boring & bore welding?
Send the scope, the machine or the volume. You will get a straight answer on whether we can do it, when, and what it costs.
Breakdowns are answered 24 hours a day, every day of the year.