Structural Repair & Fabrication
Crack repair, wear-plate renewal, bucket and body rebuilds, and fabricated equipment built to drawing.
What the work involves
Structures on mining plant crack. Booms, chassis, bins and buckets carry cyclic loads their whole life, and the repair matters as much as the weld. Cracks are ground out, prepared, welded to a documented procedure and, where the load path warrants it, reinforced rather than simply filled.
Wear management is the other half: liner and wear-plate renewal on buckets, bins and chutes, with the plate specified to the abrasion actually seen rather than to whatever is in stock.
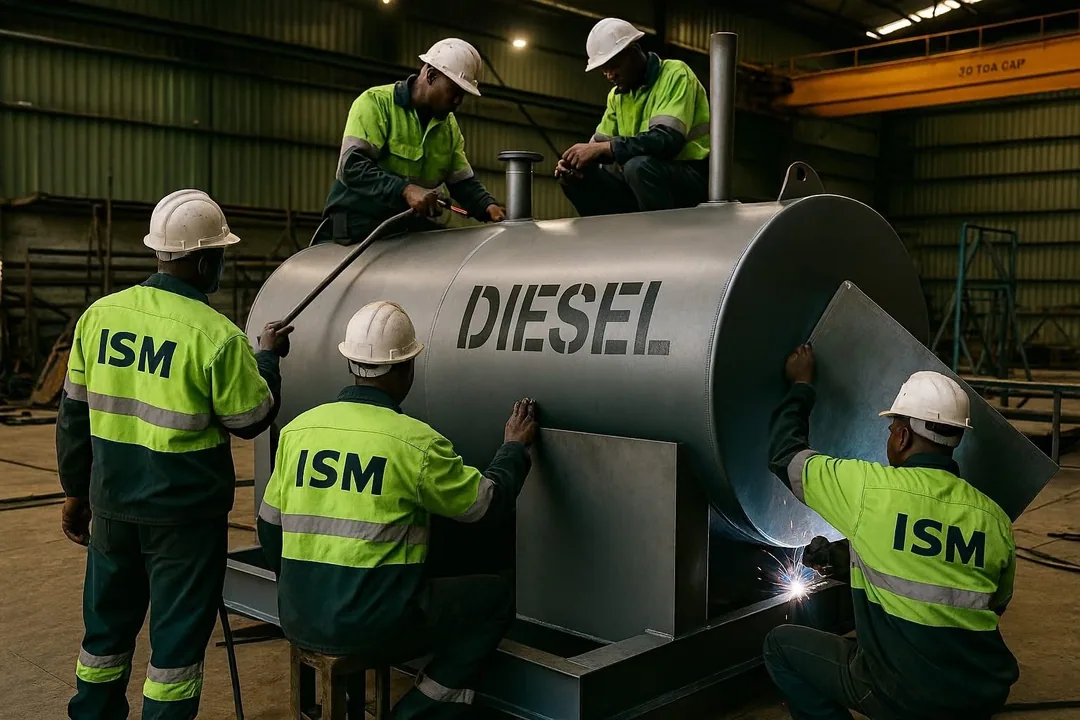
The fabrication bay also builds to drawing — diesel bowsers, service bodies, skids, stands and site equipment — with materials certified and welds carried out by coded welders.
- Division
- Heavy Mechanical
- Availability
- Workshop and on site
- Method steps
- 4
- Sectors served
- 5
- Base
- Middelburg
What this actually changes for your operation
Repairs to a written procedure
Preparation, consumable, pass sequence and pre-heat are specified per repair rather than left to the welder on the day.
Reinforced where the load says so
A crack that keeps returning is a design problem. Where the load path warrants it, we reinforce instead of re-welding the same seam.
Wear plate matched to the duty
Plate grade is specified to the abrasion actually seen on your material, which is what makes a liner last its intended life.
Built to drawing, certified
Fabricated equipment is built to drawing with material certificates and coded welders, and handed over with the documentation.
How the work runs, step by step
- 01
Inspection and crack detection
1 dayAffected area cleaned and inspected, with dye-penetrant or magnetic-particle testing to establish the true extent.
- 02
Repair procedure
1–2 daysPreparation, consumable, pre-heat and pass sequence specified in writing before any arc is struck.
- 03
Execution
Per scopeCrack ground out and welded to procedure by coded welders, with reinforcement added where the load path requires it.
- 04
Verification and finish
1–2 daysRepair re-tested, dressed, primed and painted, with the procedure and test results handed over.
What we bring to it
MIG, MMA and gouging plant
Structural welding and carbon-arc preparation
Plate rolling and cutting
Profile cutting and forming for liners and bodies
Overhead lifting
Rated handling of bodies, buckets and fabricated assemblies
NDT equipment
Dye-penetrant and magnetic-particle crack detection
Pre-heat equipment
Controlled pre-heat and interpass temperature on heavy sections
What is in place before work starts
Hot work permits, fire watch and gas testing before any cutting or welding
Fume extraction and respiratory protection in the fabrication bays
Structures supported and cribbed before load-bearing members are cut
Confined-space controls where work is inside a bin, tank or body
Where this service is used
Usually bought alongside
Need structural repair & fabrication?
Send the scope, the machine or the volume. You will get a straight answer on whether we can do it, when, and what it costs.
Breakdowns are answered 24 hours a day, every day of the year.